
A titanium pivot axle asks the process engineer to manage more than the final diameter. Tool condition, support, chip removal and heat all need to be considered in the actual operation. The useful manufacturing explanation links those choices to the features the drawing requires, instead of presenting a universal cutting recipe.
For an OEM team, TC4 titanium fastener machining becomes useful when Start with the, Explain tool-edge and, Manage heat and and Support slender and are tied to one component or purchase decision. This guide follows the six stages in the source framework and keeps manufacturing, inspection and delivery assumptions visible as the project moves forward.
The TC4 titanium fastener machining examples are planning methods, not universal acceptance values. Apply them to the released bicycle platform, mating parts and approved validation plan, and keep any open field identified until the responsible team closes it.
Start with the material and part definition
Start with the current part, assembly or order state rather than a blank specification. For TC4 titanium fastener machining, this means the team should start with the material and part definition with Start with the visible in the discussion. The purpose is to connect the article topic to an actual bicycle component, hardware family or purchase order rather than treat the heading as a general capability claim.
Place Start with the, Explain tool-edge and, Manage heat and and Support slender and in the same working record. A change to one field can alter machining access, final fit, inspection effort, batch planning or the delivered condition. The immediate output is a start with the material and part definition record that states the current revision, the proposed change and the point that still needs approval.
The first record should show what is known, what is assumed and which decision the project team needs next. In a practical tc4 titanium fastener machining review, engineering should explain the functional reason, purchasing should confirm quantity and supplied scope, and manufacturing should identify the route or information needed to proceed. The team can then compare alternatives without mixing an unapproved proposal into the released requirement.
For a prototype or first order, write one or two questions that the part, report or delivery can answer. Keep the result with the relevant drawing, material and finish state. If geometry, quantity, processing or assembly changes later, reopen the stage 1 working record for the affected configuration rather than extending the earlier conclusion without review.
Explain tool-edge and chip behavior
Translate the requirement into feature-level inputs that design, purchasing and manufacturing can all read. For TC4 titanium fastener machining, this means the team should explain tool-edge and chip behavior with Explain tool-edge and visible in the discussion. The purpose is to connect the article topic to an actual bicycle component, hardware family or purchase order rather than treat the heading as a general capability claim.
Place Manage heat and, Support slender and, Control threads and and Make batch production in the same working record. A change to one field can alter machining access, final fit, inspection effort, batch planning or the delivered condition. The immediate output is a explain tool-edge and chip behavior record that states the current revision, the proposed change and the point that still needs approval.
This is where an attractive concept becomes a controlled drawing, process question or supply definition. In a practical tc4 titanium fastener machining review, engineering should explain the functional reason, purchasing should confirm quantity and supplied scope, and manufacturing should identify the route or information needed to proceed. The team can then compare alternatives without mixing an unapproved proposal into the released requirement.
For a prototype or first order, write one or two questions that the part, report or delivery can answer. Keep the result with the relevant drawing, material and finish state. If geometry, quantity, processing or assembly changes later, reopen the stage 2 working record for the affected configuration rather than extending the earlier conclusion without review.
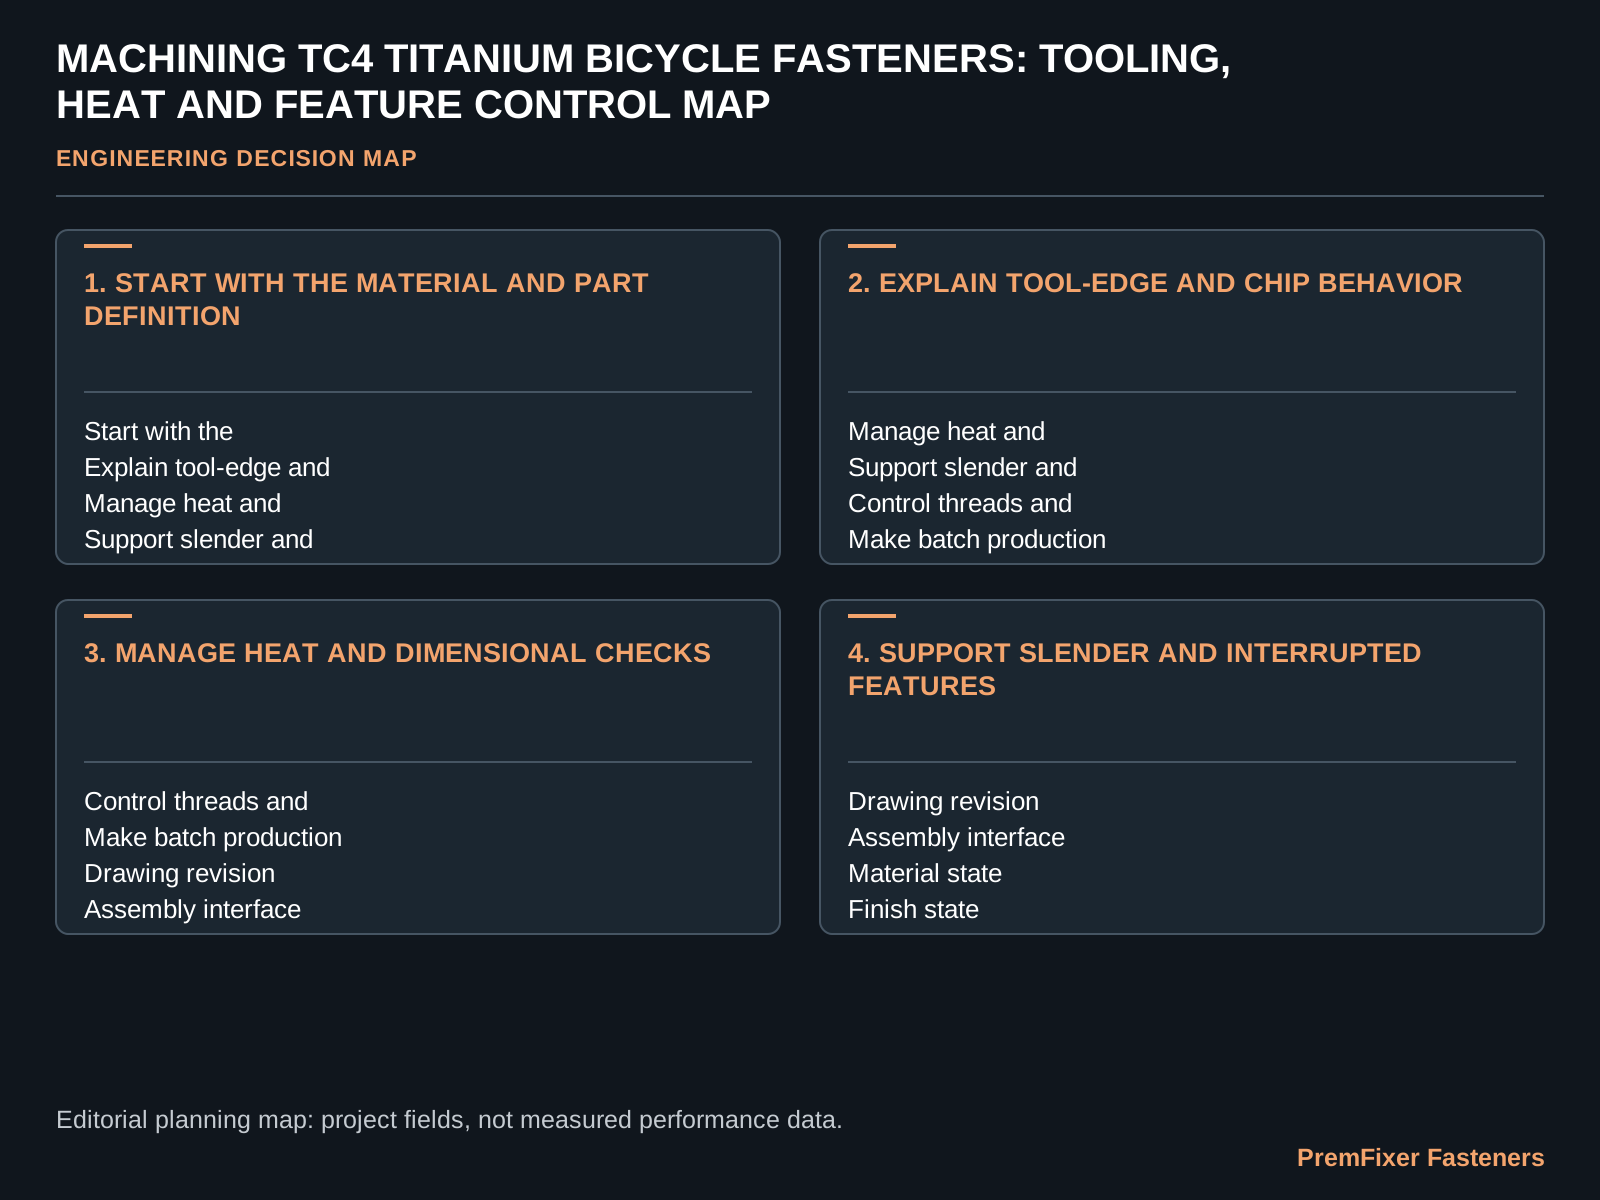
| Stage | Project decision | Inputs to connect | Working output |
|---|---|---|---|
| 01 | Start with the material and part definition | Start with the / Explain tool-edge and / Manage heat and | start with the material and part definition record |
| 02 | Explain tool-edge and chip behavior | Manage heat and / Support slender and / Control threads and | explain tool-edge and chip behavior record |
| 03 | Manage heat and dimensional checks | Control threads and / Make batch production / Drawing revision | manage heat and dimensional checks record |
| 04 | Support slender and interrupted features | Drawing revision / Assembly interface / Material state | support slender and interrupted features record |
| 05 | Control threads and surface quality | Material state / Finish state / Order quantity | control threads and surface quality record |
| 06 | Make batch production repeatable | Order quantity / Inspection method / Delivery scope | make batch production repeatable record |
Manage heat and dimensional checks
Connect the selected option to the machining route and the interfaces that the finished part must serve. For TC4 titanium fastener machining, this means the team should manage heat and dimensional checks with Manage heat and visible in the discussion. The purpose is to connect the article topic to an actual bicycle component, hardware family or purchase order rather than treat the heading as a general capability claim.
Place Control threads and, Make batch production, Drawing revision and Assembly interface in the same working record. A change to one field can alter machining access, final fit, inspection effort, batch planning or the delivered condition. The immediate output is a manage heat and dimensional checks record that states the current revision, the proposed change and the point that still needs approval.
A sample should answer a named question instead of acting as a general promise about future production. In a practical tc4 titanium fastener machining review, engineering should explain the functional reason, purchasing should confirm quantity and supplied scope, and manufacturing should identify the route or information needed to proceed. The team can then compare alternatives without mixing an unapproved proposal into the released requirement.
For a prototype or first order, write one or two questions that the part, report or delivery can answer. Keep the result with the relevant drawing, material and finish state. If geometry, quantity, processing or assembly changes later, reopen the stage 3 working record for the affected configuration rather than extending the earlier conclusion without review.
Support slender and interrupted features
Define how the result will be checked and which revision or lot the record belongs to. For TC4 titanium fastener machining, this means the team should support slender and interrupted features with Support slender and visible in the discussion. The purpose is to connect the article topic to an actual bicycle component, hardware family or purchase order rather than treat the heading as a general capability claim.
Place Drawing revision, Assembly interface, Material state and Finish state in the same working record. A change to one field can alter machining access, final fit, inspection effort, batch planning or the delivered condition. The immediate output is a support slender and interrupted features record that states the current revision, the proposed change and the point that still needs approval.
The measurement or review method must evaluate the relationship described by the drawing and assembly. In a practical tc4 titanium fastener machining review, engineering should explain the functional reason, purchasing should confirm quantity and supplied scope, and manufacturing should identify the route or information needed to proceed. The team can then compare alternatives without mixing an unapproved proposal into the released requirement.
For a prototype or first order, write one or two questions that the part, report or delivery can answer. Keep the result with the relevant drawing, material and finish state. If geometry, quantity, processing or assembly changes later, reopen the stage 4 working record for the affected configuration rather than extending the earlier conclusion without review.
Control threads and surface quality
Carry the engineering decision into batch, assembly, service or delivery planning. For TC4 titanium fastener machining, this means the team should control threads and surface quality with Control threads and visible in the discussion. The purpose is to connect the article topic to an actual bicycle component, hardware family or purchase order rather than treat the heading as a general capability claim.
Place Material state, Finish state, Order quantity and Inspection method in the same working record. A change to one field can alter machining access, final fit, inspection effort, batch planning or the delivered condition. The immediate output is a control threads and surface quality record that states the current revision, the proposed change and the point that still needs approval.
This prevents a technically sound decision from being lost when quantities, operators or suppliers change. In a practical tc4 titanium fastener machining review, engineering should explain the functional reason, purchasing should confirm quantity and supplied scope, and manufacturing should identify the route or information needed to proceed. The team can then compare alternatives without mixing an unapproved proposal into the released requirement.
For a prototype or first order, write one or two questions that the part, report or delivery can answer. Keep the result with the relevant drawing, material and finish state. If geometry, quantity, processing or assembly changes later, reopen the stage 5 working record for the affected configuration rather than extending the earlier conclusion without review.
Make batch production repeatable
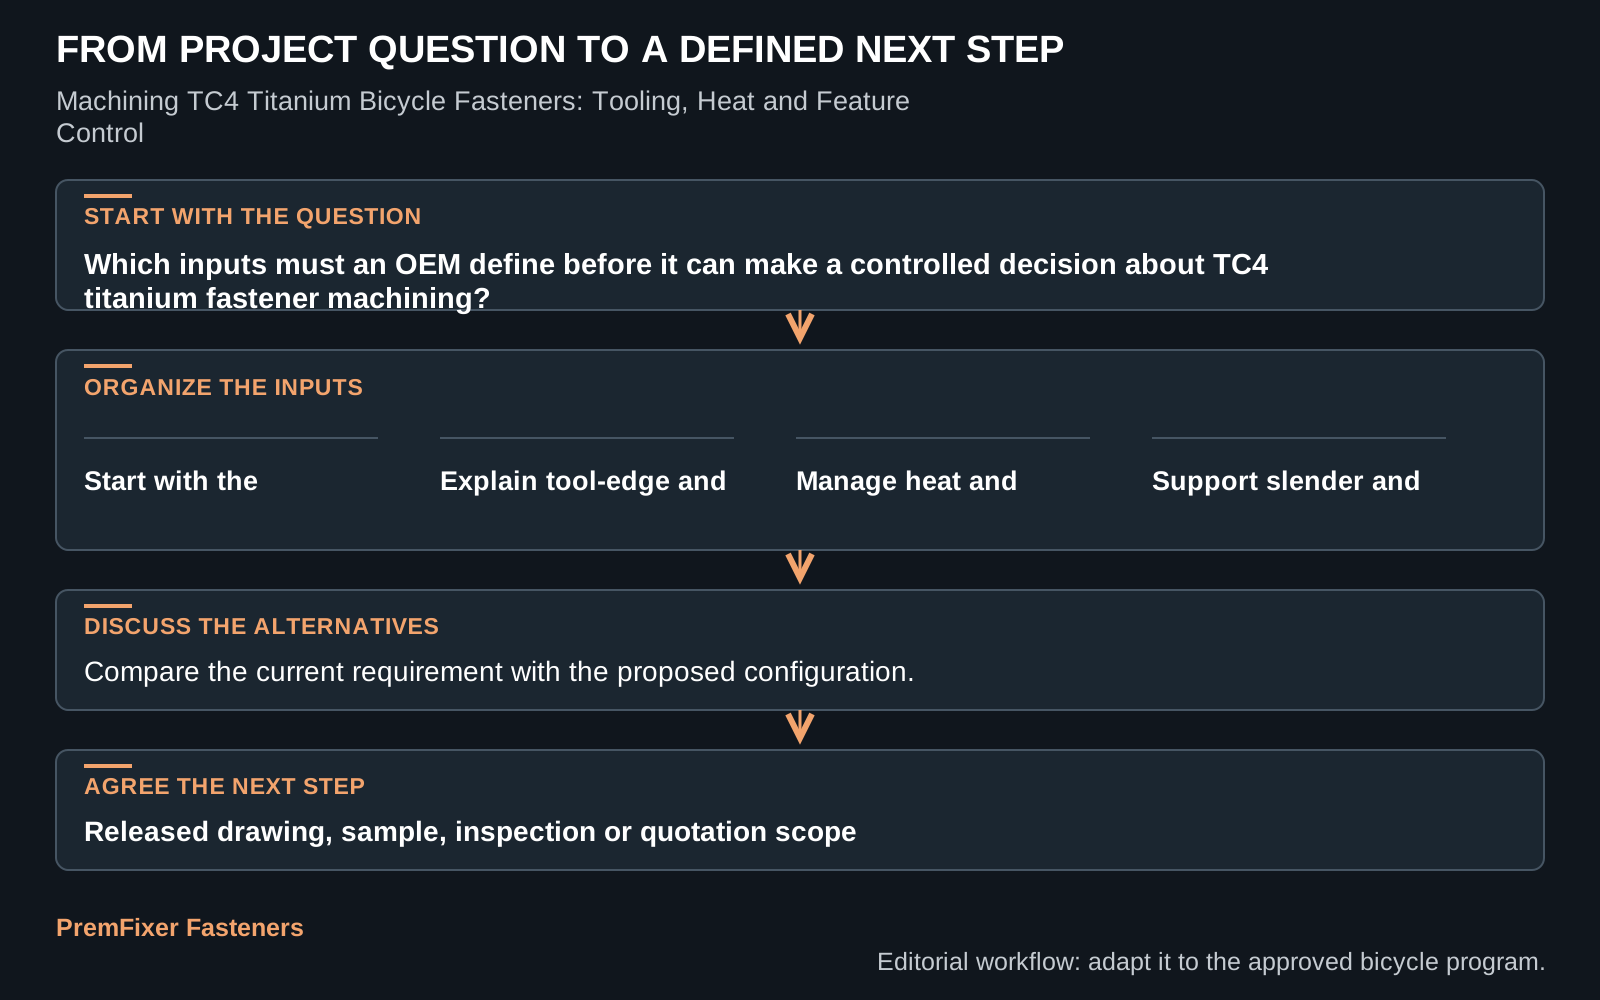
Close the topic with a release-ready project package and one responsible owner for each open point. For TC4 titanium fastener machining, this means the team should make batch production repeatable with Make batch production visible in the discussion. The purpose is to connect the article topic to an actual bicycle component, hardware family or purchase order rather than treat the heading as a general capability claim.
Place Order quantity, Inspection method, Delivery scope and Start with the in the same working record. A change to one field can alter machining access, final fit, inspection effort, batch planning or the delivered condition. The immediate output is a make batch production repeatable record that states the current revision, the proposed change and the point that still needs approval.
The supplier can then quote or plan work against a visible scope while the OEM retains approval of the final application. In a practical tc4 titanium fastener machining review, engineering should explain the functional reason, purchasing should confirm quantity and supplied scope, and manufacturing should identify the route or information needed to proceed. The team can then compare alternatives without mixing an unapproved proposal into the released requirement.
For a prototype or first order, write one or two questions that the part, report or delivery can answer. Keep the result with the relevant drawing, material and finish state. If geometry, quantity, processing or assembly changes later, reopen the stage 6 working record for the affected configuration rather than extending the earlier conclusion without review.
Questions buyers ask
What should be specified before machining TC4 hardware?
State the material requirement, condition, product form and the approved part geometry. Add finishing and inspection expectations. The name TC4 starts the material discussion, but it does not replace the full manufacturing definition or establish that another titanium specification may be substituted without review.
Why does tool condition matter in titanium machining?
Tool condition and cutting-edge behavior can affect the stability and surface outcome of the operation. Discuss the actual tool, support and chip-control arrangement rather than relying on a generic titanium capability statement. The process should connect these choices to the features being produced and inspected.
Can one cutting-speed table be used for every titanium bolt?
No. Suitable parameters depend on the material condition, tool, operation, setup and feature geometry. Use the tool supplier’s relevant guidance as a starting point for the actual process. Do not present a universal speed, feed or coolant value as a guarantee for all custom titanium fasteners.
Does room-temperature control remove all machining heat effects?
No. Environmental control and heat generated during cutting are different parts of the process. Consider the workpiece, tool and machine condition as well as the measurement state. A controlled room does not automatically make a hot, freshly machined part directly comparable with an equilibrated inspection sample.
What makes a slender titanium axle a distinct machining task?
Its geometry can affect support, tool access and the sequence used to establish the required features. Review the actual drawing rather than assuming the same setup used for a short, rigid component applies. Any proposed process or geometry change should remain tied to the approved functional requirements.
Turn the TC4 Titanium Fastener Machining Question into a Controlled RFQ
Send PremFixer Fasteners the titanium part drawing, material specification and production quantities to discuss a route tied to the actual geometry and finished requirements.
Discuss the RFQ